


News & Exhibitions
Latest Factory Updates, Industry Trends & Global Exhibition Information
Where should sanding fit in a wooden door production process?
Where should sanding fit in a wooden door production process?
Where sanding belongs in a wooden door production line depends on substrate construction, machining requirements, and the finishing system—not simply on where a sander fits on the factory floor. Effective wooden door process planning distinguishes calibration sanding from surface preparation and intercoat sanding, assigning each stage a clear purpose and measurable quality criteria. For technical evaluators, the key is to match sanding operations to upstream tolerances and downstream coating requirements. This article examines how to position these stages to control thickness, protect veneers, reduce rework, and maintain consistent throughput.
The practical answer is that sanding usually belongs at several points, but not every door needs every operation. A solid timber door, a veneered flush door, and a routed MDF door should not follow an identical sanding route. Treating them alike can mean unnecessary material removal in one product and insufficient preparation in another.
Separate thickness control from finish preparation
Calibration sanding establishes a controlled thickness and reduces limited surface variation. It belongs where downstream operations need a consistent reference surface. Typical considerations include core preparation before decorative facing and thickness correction of suitable solid wood components before subsequent machining or assembly.
Surface preparation has a different purpose: removing machining marks, adhesive residue, raised fibers, and previous abrasive scratches so the substrate is ready for the specified finish. It should remove only the material necessary to reach that condition. Using this stage to correct a major thickness error is particularly risky on thin veneer.
Intercoat sanding works on a coating rather than the original substrate. Depending on the finishing system, it may remove dust nibs, level raised grain, or provide the surface condition required for the next coat. Whether it is necessary—and when it can occur—must follow the coating supplier’s technical instructions.
These distinctions should appear on the process route. “Sand door” is not a sufficient instruction. Each operation needs an incoming condition, a removal limit where relevant, and an outgoing acceptance criterion.
Build the sequence around the door construction
For a veneered flush door, a practical starting route is: prepare and calibrate the core where required, clean the bonding surfaces, apply the facing, press, allow the adhesive assembly to stabilize, trim and machine, then carry out controlled finish sanding before coating. Sanding may be split around machining if handling or tool access makes that necessary.
The important decision is to correct core geometry before applying an expensive decorative surface. After veneering, the available sanding allowance is constrained by actual veneer thickness, previous processing, and local surface variation. Nominal veneer thickness alone does not establish a safe removal budget.
Solid wood frame-and-panel doors often need component sanding before assembly because panel edges, molded details, and internal corners become less accessible afterward. Post-assembly sanding can blend joints and prepare exposed faces, but it should not be expected to correct poorly aligned joints. Seasonal movement also means the panel must retain its designed freedom of movement.
For routed MDF doors, face sanding and profile preparation are separate tasks. Routing exposes a different surface structure from the factory-pressed face, and those areas may absorb coating differently. Profiles need suitable abrasives and contact tools; a flat-panel sander cannot prepare recessed details simply by increasing pressure.
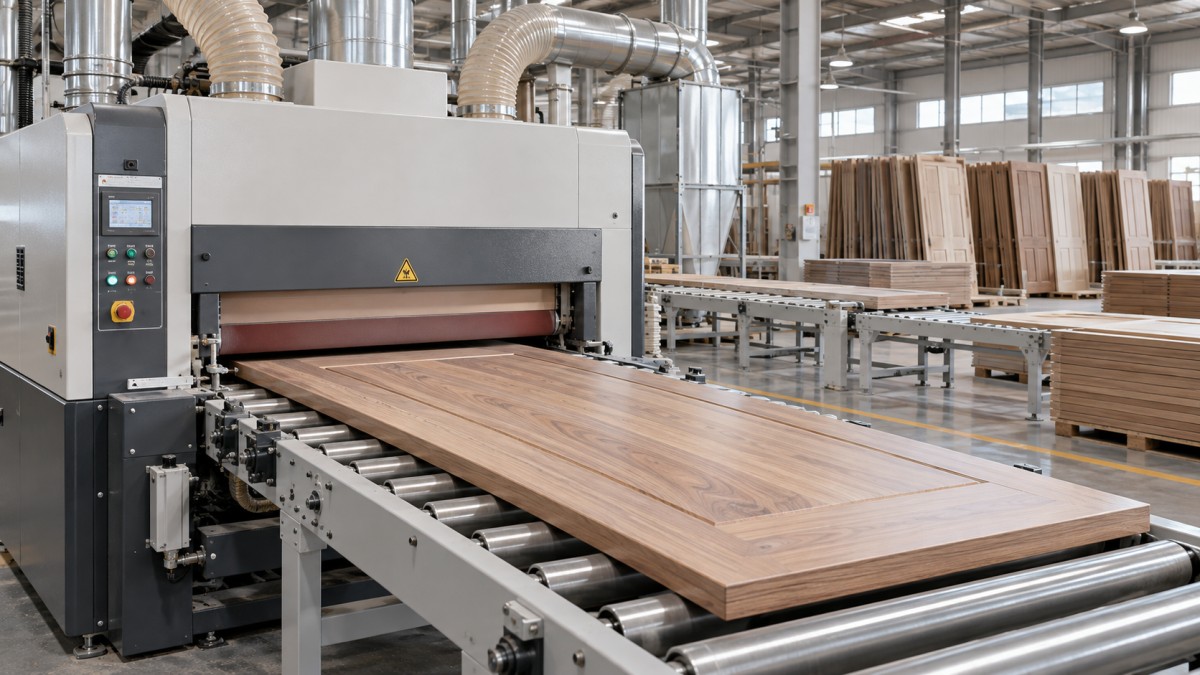
For any construction, identify which surfaces become inaccessible after assembly and which operations will create fresh defects. That establishes whether sanding should occur before assembly, after machining, or at both points.
Do not sand around an unstable upstream process
A sander can remove material; it cannot reliably repair an unstable door blank. Moisture imbalance, inadequate adhesive cure, uneven pressing, and construction-related stress can produce dimensional changes after an apparently acceptable sanding pass. This is why release conditions from pressing and conditioning matter as much as the sander settings.
Set those conditions using the adhesive specification, substrate requirements, and actual factory environment. A fixed waiting time copied from another production line may not transfer to a different adhesive, panel build-up, or temperature. Where stability is uncertain, compare dimensions before sanding and after a representative holding period.
Flatness and thickness also need separate checks. A door can have reasonably consistent thickness while remaining bowed. Some sanding arrangements may temporarily flatten a flexible blank under pressure, only for the bow to return after discharge. Measure the unloaded part on an appropriate reference setup rather than accepting machine passage as proof of flatness.
Adhesive squeeze-out deserves upstream attention too. Preventing and removing it appropriately is safer than trying to sand through hardened deposits on a delicate face. Residual adhesive can remain difficult to see until stain reveals uneven absorption.
Place final substrate sanding after the last damaging operation
Final substrate sanding should normally follow operations that can leave visible marks on the surfaces being finished. These may include trimming, routing, lock preparation, handling, and local repairs. However, the sequence is not absolute: machining a prefinished door may be intentional, provided exposed areas receive the required subsequent treatment.
Consider edges explicitly. Face sanding does not remove cutter marks from door edges, hinge recesses, or molded profiles. Edge rounding must also be controlled against the drawing and coating specification. Excessive rounding can change appearance and fit, while an unsuitable sharp edge may be difficult to coat consistently.
Abrasive selection should follow the substrate and finish, not a universal grit recipe. The starting abrasive must remove the preceding defect efficiently; subsequent steps must remove its scratch pattern. Overly coarse sanding leaves scratches that transparent finishes may emphasize. Excessively fine preparation can alter stain uptake and may conflict with the coating supplier’s recommendations.
Validate the sequence on representative doors using the intended stain, sealer, and topcoat. Inspecting bare wood alone is insufficient because wetting, color, and sheen reveal defects differently. Record the abrasive grading system as well as the grit designation so replacement consumables remain comparable.
Keep coating preparation and intercoat sanding under separate control
After final substrate sanding, remove dust without introducing oil, moisture, or incompatible cleaning residues. Compressed air is not automatically clean, and blowing dust off one door can contaminate the next. Extraction and cleaning arrangements should prevent sanding dust from migrating into coating areas.
Intercoat sanding must wait until the coating reaches its specified sandable condition. Sanding too early can cause loading, smearing, or tearing rather than clean abrasion. Dry-to-touch and ready-to-sand are not interchangeable release criteria.
The required abrasion also depends on the recoat window. Some systems allow another coat without sanding under defined conditions; others require mechanical preparation. Do not add intercoat sanding automatically, particularly between color layers where abrasion could disturb appearance.
Where sanding is required, control cut-through at edges and high spots, then clean and inspect before recoating. If cut-through occurs, use an approved repair procedure rather than assuming the next coat will hide it.
Turn sanding quality into measurable acceptance conditions
Useful wooden door process planning links each sanding stage to evidence that production staff can check. The acceptance criteria should come from the product drawing, surface specification, adhesive requirements, and finishing documentation—not from arbitrary machine settings.
- Calibration: measure thickness at defined locations and check unloaded flatness separately. Confirm sufficient material remains for subsequent operations.
- Veneer preparation: inspect for breakthrough, local thinning, open joints, and residual adhesive. Control cumulative removal across repeated passes and rework.
- Pre-coating preparation: assess scratches and machining marks under consistent lighting, then confirm appearance with an approved finished sample.
- Intercoat preparation: verify the coating’s sandable condition, adequate defect removal, and absence of exposed substrate or damaged color.
Keep visual reference samples for acceptable and unacceptable surfaces. A roughness measurement can support control, but it does not fully describe scratch direction, isolated defects, or how a stain will look. Likewise, belt speed, feed speed, and pressure are process settings—not evidence that the surface meets specification.
Evaluate the sanding cell as part of the whole line
Machine selection should follow the process map. Compare working width, workpiece thickness range, contact arrangement, feed stability, profile access, and adjustment repeatability against the actual door mix. Thin decorative faces demand controlled contact and removal; recessed profiles require tools that can reach them without erasing detail.
Capacity assessment must include belt changes, cleaning, inspection, product changeovers, and rework—not just nominal feed speed. Provide suitable buffers where pressing or coating release times differ from sanding throughput. Extraction capacity and combustible-dust controls require assessment against the machinery documentation and applicable local safety requirements.
Qingdao Zhongding Machinery Co., Ltd., a woodworking machinery manufacturer and exporter with more than 20 years of industry experience, can contribute to this equipment-and-process discussion. Its stated support scope includes technical assistance, spare parts supply, and after-sales service. During evaluation, make those capabilities concrete by confirming commissioning responsibilities, abrasive availability, wear-part identification, and troubleshooting support for the proposed configuration.
Before approving the layout, run representative door constructions through the proposed sequence and complete the intended finish. Record incoming variation, sanding removal, surface acceptance, and changeover requirements. The right location for sanding is the point where it corrects a defined condition without compromising the next operation—not simply the available space between two machines.
Send Your Inquiry
We welcome your cooperation and we will develop with you.