


News & Exhibitions
Latest Factory Updates, Industry Trends & Global Exhibition Information
Why does a CNC boring machine produce misaligned dowel holes?
A CNC boring machine produces misaligned dowel holes when the programmed coordinates, the panel’s actual position, and the drill’s cutting path do not agree. The same assembly failure can result from an incorrect datum, a reversed part, panel movement, drill deflection, or a drilling head that is no longer square. Replacing a spindle or adjusting axis compensation before separating these causes can leave the original fault unresolved.
The most useful initial distinction is whether the error is repeatable, changes across the panel, or appears only after assembly. A consistent displacement points toward a reference or offset problem; scattered positions suggest unstable seating or cutting conditions. Holes that measure correctly at the surface but resist dowel insertion require checks for drilling angle, diameter, and depth—not just X/Y positioning.
Confirm that the holes are actually misplaced
A joint that will not close is not sufficient evidence of a positioning fault. An undersized hole, an oversized or swollen dowel, trapped chips, or insufficient drilling depth can prevent assembly even when both hole centers are correct. Excess glue in a blind hole can also obstruct full insertion.
Inspect both mating components before changing machine settings. Measure hole position from the intended assembly reference edge, then check hole diameter, usable depth, panel thickness, and edge squareness. Distinguish the programmed drilling depth from the usable cylindrical depth left behind by the drill tip.
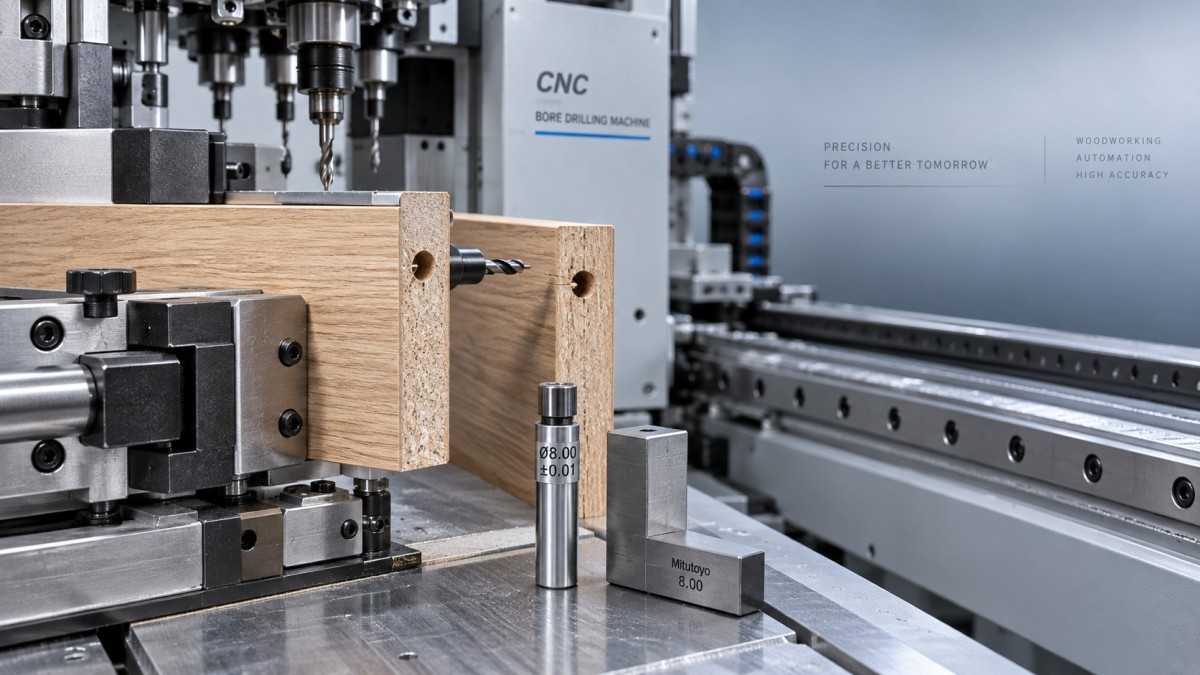
For a clean, round hole, a suitable close-fitting gauge pin can make center-position measurement more reliable than measuring a torn hole edge. Account for half the pin diameter when calculating the center. A loose pin or an oval hole makes this method unreliable. Check assembly with verified dowels and without glue to separate geometric interference from bonding-related problems.
Preserve a rejected pair, identify its mating faces, and mark the machine reference edges. Also record the program revision, tool station, panel orientation, and whether the defect began after a tool change, collision, maintenance operation, or software update. These details narrow the investigation without altering the evidence.
Read the error pattern before adjusting anything
Record actual position minus specified position for each hole, using consistent coordinate directions. Do not compare measurements taken from different physical edges unless they have been converted to the same assembly datum.
These patterns establish test priorities, not final diagnoses. A displaced locating stop and a wrong work offset can produce nearly identical results. The deciding evidence is whether the physical reference or the coordinate definition is incorrect.
Separate repeatability from accuracy
Run a simple diagnostic pattern on flat, dimensionally checked scrap using an approved test program. Include holes at separated positions rather than clustering them near one corner. Use known-good tooling and keep material, feed, speed, and clamping conditions unchanged.
Where the machine’s operating procedure permits, repeat the pattern on separate unused locations while keeping the panel clamped. Then repeat on equivalent panels that are unloaded and reloaded between cycles. Do not re-enter existing holes to assess positioning: the previous bore can guide the drill and conceal an error.
If results are consistent without unloading but vary after reloading, investigate locating surfaces, stops, loading technique, and clamp engagement. If results vary without unloading, check whether the panel moves during drilling before attributing the fault to axis repeatability. Cutting load, loose tooling, and intermittent mechanical movement remain possible causes.
Consistent results are not necessarily accurate results. A machine can reproduce the same incorrect offset on every cycle. Compare the test pattern with an independent dimensional reference and the manufacturer’s specified acceptance conditions.
Trace the reference chain from drawing to panel
A hole location passes through several coordinate systems: the drawing, machining software, postprocessor, controller work offset, drilling-head offset, and physical panel reference. A mismatch anywhere in that chain can move an otherwise accurate drilling operation.
Check the actual controller program against the approved drawing, not only the CAM preview. Confirm units, origin location, selected face, drilling direction, panel dimensions, and any rotation or mirror transformation. A correct preview does not prove that the postprocessed program uses the correct machine convention.
Opposing parts require particular care. Two panels that form a left-hand and right-hand assembly may need mirrored coordinates rather than identical coordinates. When parts are turned over for another operation, the loading orientation must agree with the program’s face definition.
Thickness references can create less obvious errors in edge drilling. If the intended hole center is on the panel mid-plane, a difference between actual and entered thickness can shift the center relative to that intended plane. The result depends on whether the machine references the top face, bottom face, or measured center. Verify that logic rather than assuming the controller automatically compensates for thickness.
Also measure panel size and squareness. Holes located correctly from opposite edges may fail to mate when the panels have different actual dimensions. On solid-wood parts, confirm that the dimensions at machining and assembly remain comparable; do not compensate the machine for a workpiece that has changed shape.
Check locating and clamping under drilling load
Dust against a locating stop, a damaged fence, or a chip beneath a panel changes the physical datum. Clean and inspect these contact surfaces before recalibrating offsets. Confirm that stops return fully and that movable locating devices lock securely.
A panel can appear secure while remaining able to slide or rotate. Horizontal boring applies lateral force, so adequate downward pressure alone does not guarantee resistance to movement. Verify clamp placement, pad condition, support near the drilling edge, and pressure during the cycle—not merely the static gauge reading.
For vacuum-held parts, inspect seals, unused suction openings, support surfaces, and material permeability. For pneumatically clamped machines, examine supply stability, leaks, pressure regulation, and the timing between clamp confirmation and drilling engagement. A confirmation signal may establish actuator position without proving that the panel is firmly seated.
Excess clamping force is not a universal remedy. It can bend a thin or bowed panel against the table; after release, the panel springs back and changes the relationship between the holes and assembly surfaces. Correct support and restraint are preferable to using clamp pressure to conceal poor flatness.
Distinguish a displaced spindle from a wandering drill
If the defect is limited to one tool station, inspect that station before changing shared machine parameters. Under the prescribed isolation procedure, check the drill shank, collet or chuck, seating surfaces, holder security, and signs of impact or contamination. Confirm the specified drill diameter, projection, cutting geometry, and rotation direction.
A drill can enter at the correct coordinate and then deviate inside the material. Excessive projection reduces rigidity; a damaged cutting edge can create unequal cutting forces; poor chip evacuation increases resistance. A hole may therefore look correctly positioned at its mouth while steering the dowel away from the mating bore.
Use a compatible known-good drill to separate tool condition from spindle condition. If the fault follows the drill, investigate the tool or its setup. If it remains at the same spindle station, inspect that spindle’s holder, bearings, alignment, and configured offset. Conduct comparisons only where tool specifications and machine procedures allow interchange.
Runout and alignment are different measurements. Runout concerns rotation around the spindle axis; alignment concerns the direction and location of that axis. A low-runout spindle can still drill at an incorrect angle. Conversely, an oversized or oval hole may indicate runout or vibration without a corresponding axis-position error.
Changing feed or speed may reduce deflection, but it does not correct a tilted drilling head. Use cutting adjustments only within the tool and machine recommendations, and verify whether they address the cause rather than merely reduce its visible effect.
Investigate machine geometry when simpler causes are excluded
Mechanical checks become justified when known-good tools, verified programs, stable panels, and correct references still produce a repeatable error. Relevant checks include axis reversal behavior, guideway condition, drive couplings, screw or rack engagement, spindle-head mounting, and squareness between the motion axes and drilling directions.
An error that depends on approach direction suggests lost motion or reversal-related behavior. An error that increases across travel requires a wider positional check; it is not adequately diagnosed with a single hole near the origin. A collision can also alter head alignment without producing an obvious controller alarm.
Follow the manufacturer’s metrology procedure and use instruments suitable for the required tolerance. Check machine leveling and foundation condition where required by that procedure, particularly after relocation. Compare measurements at the specified operating condition, since a cold-machine check may not represent stabilized production behavior.
Back up parameters before any authorized adjustment. Do not use backlash compensation, scale correction, or head offsets to hide loose hardware or unstable positioning. Compensation is appropriate only for a characterized, repeatable error within the machine’s adjustment method.
Inspection inside guarded areas requires the prescribed electrical, pneumatic, and stored-energy isolation. Powered diagnostic movement should use the manufacturer’s approved service mode, with guarding and interlocks maintained as specified.
Validate the repair at the assembly, not just the controller
Change one variable at a time and repeat the same diagnostic pattern. Once the measured error is corrected, produce representative mating parts using the normal loading sequence, relevant drilling heads, panel orientations, and production tooling. Verify both dimensional results and dry assembly.
Acceptance should follow the drawing and machine specification rather than a generic dowel-hole tolerance. Available assembly clearance depends on hole and dowel diameters, engagement length, bore direction, and the combined positional error of both parts. Two individually acceptable measurements do not automatically guarantee a satisfactory joint.
Retain the before-and-after measurements, program revision, tooling details, and adjustment record. A defensible repair identifies what moved—the coordinate reference, the panel, the cutting path, or the machine geometry—and demonstrates that the same failure no longer occurs under normal production conditions.
Send Your Inquiry
We welcome your cooperation and we will develop with you.