


News & Exhibitions
Latest Factory Updates, Industry Trends & Global Exhibition Information
What should a woodworking production process consultation deliver?
A woodworking production process consultation should deliver a documented basis for deciding what to change, what to buy, and how to verify that the investment works. Procurement should leave with an agreed production baseline, a credible capacity estimate, equipment and layout requirements, and an implementation plan tied to measurable results.
The depth of that work depends on the decision. Replacing a standalone machine may require a focused assessment of its workload and interfaces. Expanding a furniture production line requires a broader review of material flow, staffing, utilities, and downstream capacity. In either case, recommendations should explain their assumptions clearly enough for the buyer to compare proposals and challenge the investment case.
A woodworking production process consultation service becomes useful when it connects the equipment quotation to the factory’s actual constraints. A machine list alone leaves procurement carrying too much of the technical and financial risk.
A production baseline that explains where output is being lost
The first deliverable should describe how production performs before any proposed changes. Without that baseline, a supplier can recommend a faster machine while leaving unanswered whether machine speed is limiting finished output.
For panel furniture, the assessment might follow boards through cutting, edge banding, drilling, assembly, and packing. For solid wood products, it may need to account for stock preparation, machining, sanding, and finishing. The route should reflect the products being made, including outsourced operations and rework loops.
Procurement should expect the consultant to request representative drawings, material specifications, order quantities, shift patterns, staffing arrangements, and production records. Product variety matters: a line processing repeated cabinet components has a different workload from a workshop producing frequently changing sizes and constructions.
The baseline should distinguish recorded performance from estimates. If reliable downtime or reject records are unavailable, the report should identify how those gaps affect confidence in the recommendation. Observation, sample timing, and discussions with operators can support an initial assessment, but they should not be presented as a fully measured production history.
A useful process map shows where material waits as well as where it is worked. Queues, repeated handling, missing components, and quality holds can restrict output even when individual machines appear to have spare capacity. Excess work in progress can also obscure which operation is causing the delay.
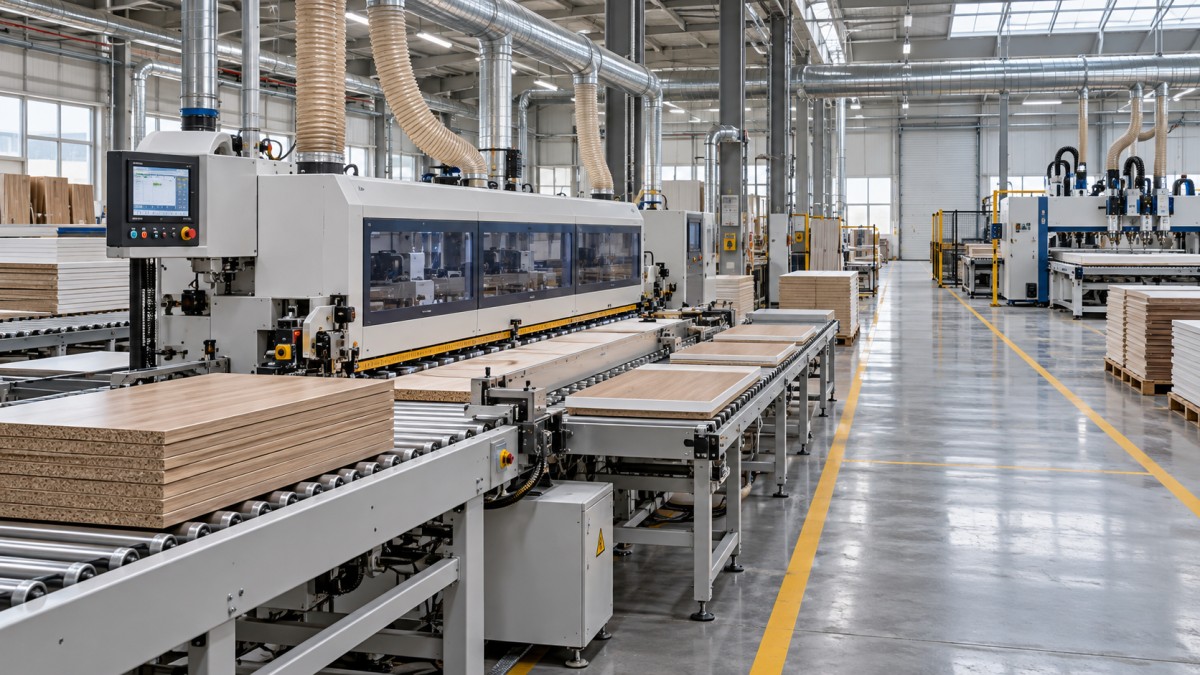
The consultation should connect each important constraint to evidence. If edge banding appears to be the bottleneck, the report should explain whether the cause is processing time, setup changes, adhesive preparation, part sequencing, or time spent correcting defects. These causes lead to different purchasing decisions.
That distinction gives procurement a way to assess the proposed remedy. More machine capacity may help a heavily loaded operation, while better scheduling, tooling, maintenance, or material presentation may address a different constraint at lower cost. The report should make those alternatives visible before committing to equipment.
Capacity estimates built around the actual product mix
A consultation should translate the production target into a capacity model that buyers can inspect. Rated feed speed or a demonstration cycle gives limited information about the number of acceptable components a factory can complete during a working shift.
The model should state its operating basis: working time, representative product mix, batch sizes, changeover frequency, staffing, and expected interruptions. It should also explain how rejects and rework affect usable output. Where these inputs are uncertain, a range of outcomes is more informative than a precise forecast built on weak assumptions.
Units need particular care. Panels cut, edges processed, holes drilled, and furniture units assembled are different measures. A proposal expressed in cabinets per shift should show how cabinet designs translate into component quantities and processing workloads. Otherwise, proposals using the same headline output may describe substantially different production requirements.
For procurement, the most useful capacity deliverable includes:
- The required workload: operations and quantities for an agreed set of representative products.
- Available processing time: the allowance for breaks, setups, maintenance, and other planned stops.
- Expected usable output: production after the stated allowances for downtime and quality losses.
- The limiting operation: the process that constrains finished output under the proposed arrangement.
- Sensitivity to change: what happens when batch sizes fall, product variety increases, or staffing is reduced.
Capacity should be checked across connected operations. Increasing cutting output can overload edge banding, drilling, or sorting. Adding a CNC machining center may create extra demand for programming, tooling preparation, and component identification. The consultation should show whether the proposed change improves finished output or simply moves the queue.
A procurement team should also ask how much operational flexibility supports the estimate. A forecast that depends on long, uninterrupted batches may be unsuitable for a business selling short runs with frequent design changes. The equipment could perform exactly as specified while the factory still misses its delivery targets.
Quality belongs in this discussion because acceptable output is the commercial objective. Dimensional accuracy, edge finish, joint fit, and surface condition should be linked to product requirements. The consultant should identify the conditions needed to achieve them, including material consistency, tooling condition, handling practices, and any intermediate inspection points.
A specification and layout that expose integration costs
The equipment recommendation should become a procurement specification with enough detail to obtain comparable quotations. It should connect machine capabilities to the intended materials, component dimensions, operations, and quality requirements. Listing model names and motor power does little to explain whether a proposed configuration fits the workload.
Options deserve particular scrutiny. Tooling packages, clamping arrangements, loading systems, measuring devices, software functions, and extraction connections can change both cost and practical capability. The consultation should distinguish what is necessary for the agreed production target from what supports a possible future expansion.
Compatibility with existing equipment should be explicit. Buyers need to understand how parts move between operations, whether reference edges and component orientation remain consistent, and whether identification survives the production route. A machine can meet its own specification yet introduce extra turning, sorting, or manual checking between stages.
Where software is involved, the deliverable should describe the path from design data to machine instructions. File compatibility alone does not establish that the workflow is ready. Post-processors, machining rules, labels, revision control, and operator responsibilities may all require attention. A representative part should be traced through that data flow before the buyer accepts broad claims about integration.
The proposed layout should likewise go beyond fitting machine footprints into a building. Procurement needs a dimensioned arrangement showing loading and unloading space, operator access, maintenance access, material storage, and the movement of components between processes. Clearances should be checked against the selected equipment and site conditions.
Utilities and installation requirements should be included in the same package. Depending on the machinery, these may cover electrical supply, compressed air, extraction, foundations, access for delivery, and lifting arrangements. Dust collection requirements should be assessed for the intended machines and materials; an available duct connection alone does not establish adequate performance.
Responsibility boundaries are especially valuable when several suppliers are involved. The consultation should identify who provides connections, guarding at interfaces, software setup, commissioning materials, and operator training. Applicable site safety and regulatory requirements should be addressed through competent assessment, with responsibilities assigned in the project scope.
These details allow procurement to compare the cost of a working installation. A lower machine price may be offset by excluded tooling, building modifications, additional handling equipment, or integration work. The consultation should make those exclusions visible while there is still time to resolve them commercially.
An investment case with a workable route to acceptance
The financial deliverable should connect spending to specific operational improvements. Relevant benefits might include additional saleable output, lower material loss, less rework, reduced overtime, or fewer handling steps. Each benefit needs a stated basis and a clear relationship to the proposed change.
Care is needed when assigning value to time savings. If automation releases operator time but staffing remains unchanged, the immediate benefit may be extra capacity or more reliable scheduling. Treating all saved minutes as a cash reduction can overstate the return. Similarly, additional capacity has value only if demand and downstream operations can use it.
Costs should extend through installation and operation. Freight, site preparation, tooling, software, training, commissioning, consumables, maintenance, and spare parts may affect the decision. The consultant should also account for the production disruption associated with removing equipment, installing replacements, and learning the new process.
A useful comparison may include keeping the existing arrangement with targeted improvements, upgrading one constrained operation, or installing a more integrated solution. Each option should be evaluated against the same production requirement. Procurement can then see what additional spending buys and which assumptions make a larger investment worthwhile.
The implementation plan should turn the preferred option into a sequence of responsibilities and readiness checks. Site preparation, equipment delivery, installation, software configuration, training, trial production, and ramp-up need to fit the factory’s delivery commitments. Where continued production is necessary, the plan should explain how that requirement affects installation and commissioning.
Acceptance criteria should be developed before the purchase order is finalized. They should define representative materials and parts, the required quality, how output will be measured, and the conditions under which the demonstration takes place. Any exclusions should be visible—for example, whether material replenishment, changeovers, or inspection time are included in the measured run.
A successful sample part establishes only part of the case. Buyers may also need evidence that the process can maintain quality over a representative run, handle the agreed product variety, and operate with the planned staffing. The scope of acceptance should match the claims used to justify the investment.
Support requirements belong in the final deliverables too. Procurement should have a clear account of training coverage, maintenance responsibilities, recommended spares, diagnostic access, and the route for resolving faults. These provisions influence how well the factory can sustain the performance demonstrated during commissioning.
When comparing consultation proposals, ask for the deliverable scope before comparing the fee. A preliminary review based on drawings and production records can be useful for screening options. A decision involving substantial capital or integration work needs evidence proportionate to the commitment, which may require site observation, material trials, or further engineering.
The final handover should let another technically competent reviewer follow the reasoning from production data to equipment selection and expected results. Assumptions, calculations, drawings, exclusions, and responsibilities should be accessible. Procurement can then issue comparable enquiries, resolve the remaining uncertainties, and make the investment conditional on performance that both buyer and supplier understand.
Send Your Inquiry
We welcome your cooperation and we will develop with you.